News

How Can Narrow Mouth Reagent Bottle Solutions Improve Pharmaceutical Packaging Reliability?

2026-07-29 0 Leave me a message

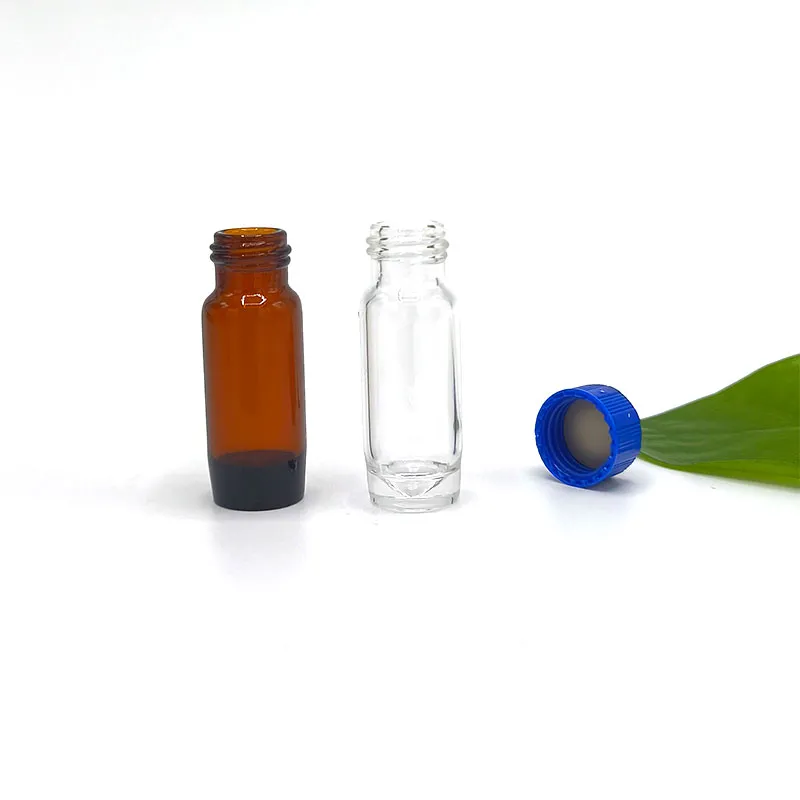
The pharmaceutical and chemical industries are experiencing continuous changes in packaging requirements. With increasing attention toward material stability, contamination prevention, and long-term storage performance, glass containers have become an essential choice for many sensitive applications. Among various laboratory packaging solutions, Narrow Mouth Reagent Bottle designs are widely recognized for their ability to provide controlled handling, reliable sealing performance, and excellent protection for chemical and pharmaceutical materials.

Modern laboratories, research institutions, and pharmaceutical manufacturers require packaging that can maintain product integrity throughout storage and transportation. Glass packaging offers strong chemical resistance, low interaction with stored substances, and excellent transparency, allowing users to monitor contents conveniently. These advantages make it an important component in scientific research, quality testing, and industrial production environments.

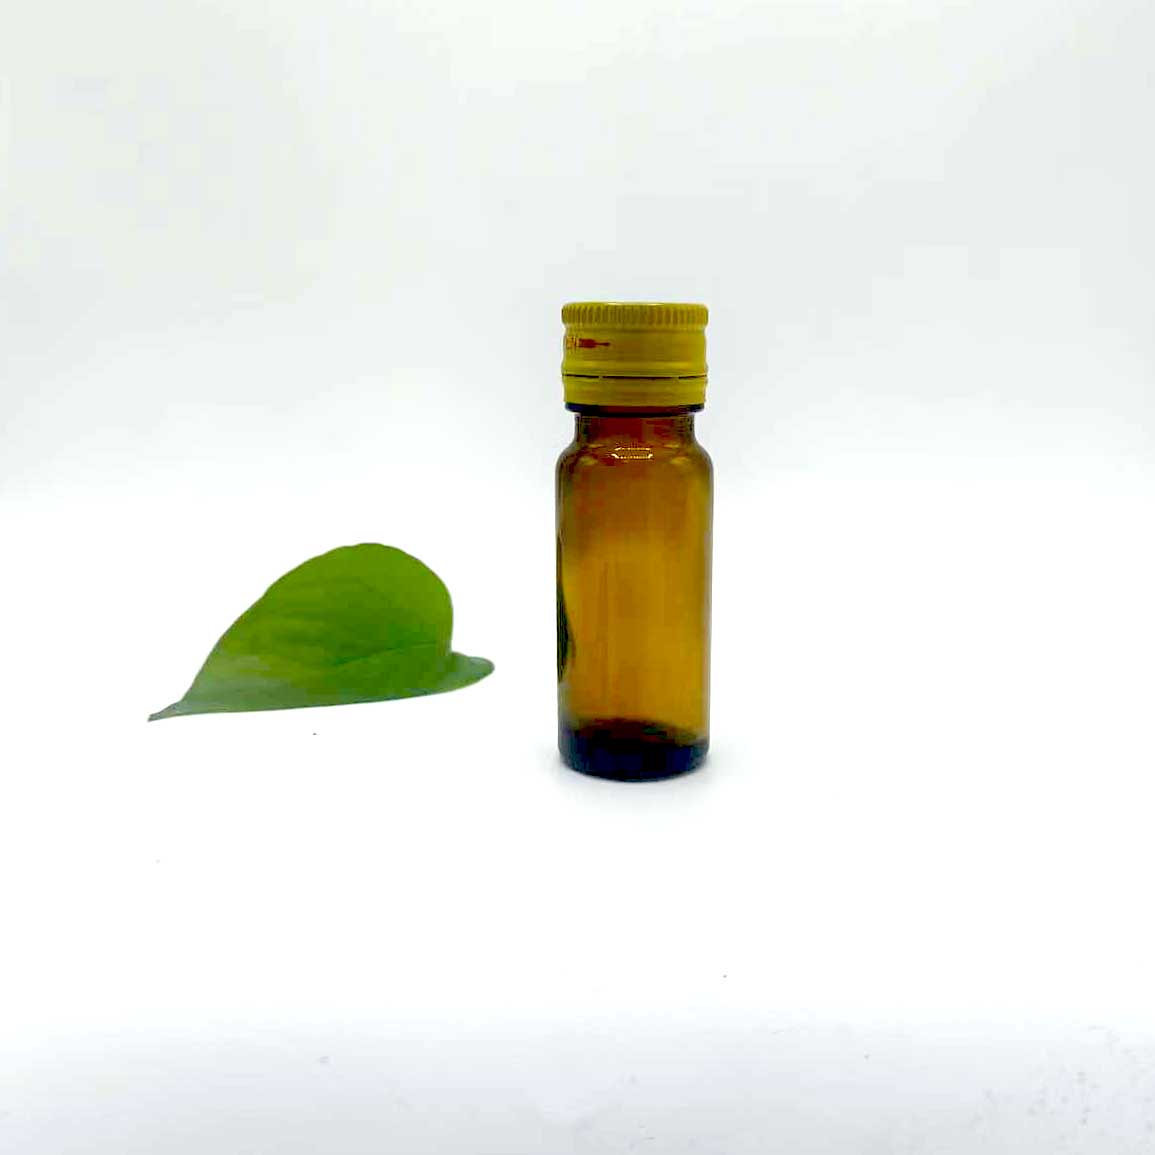
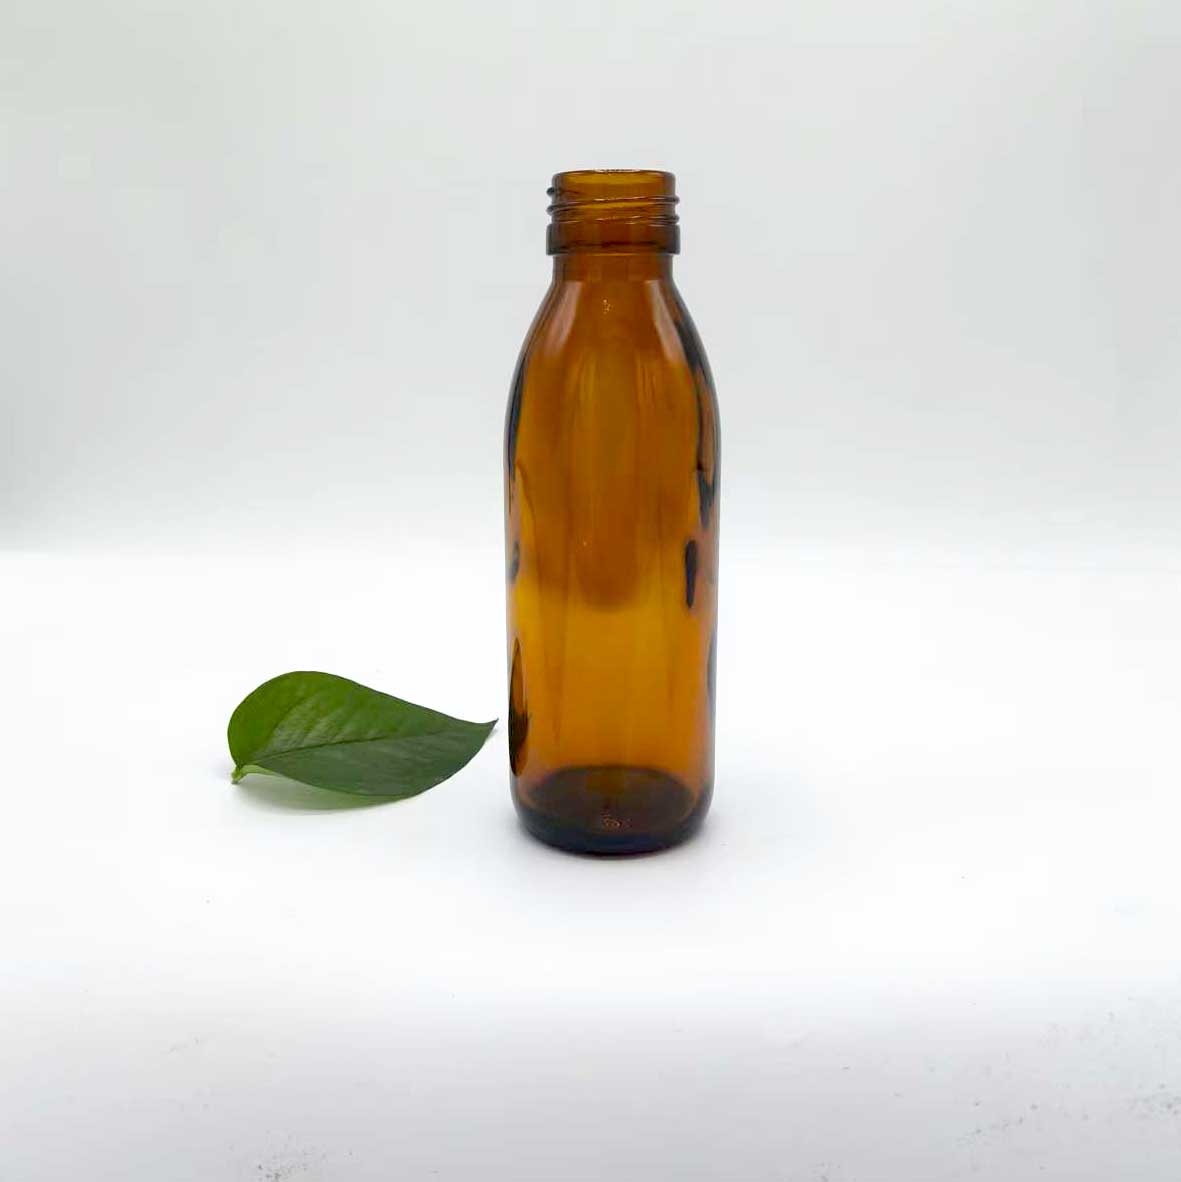
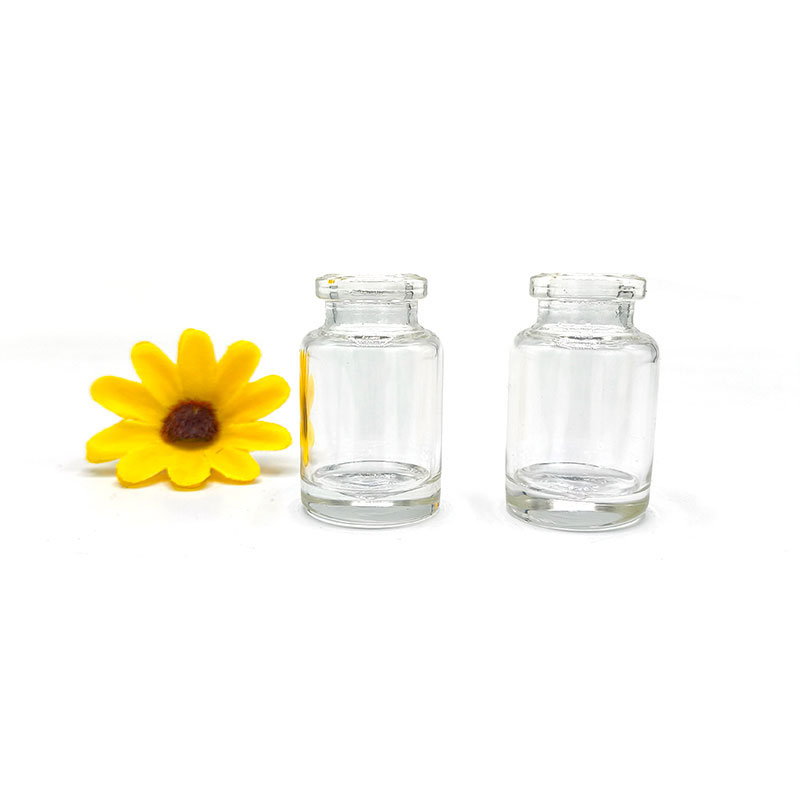
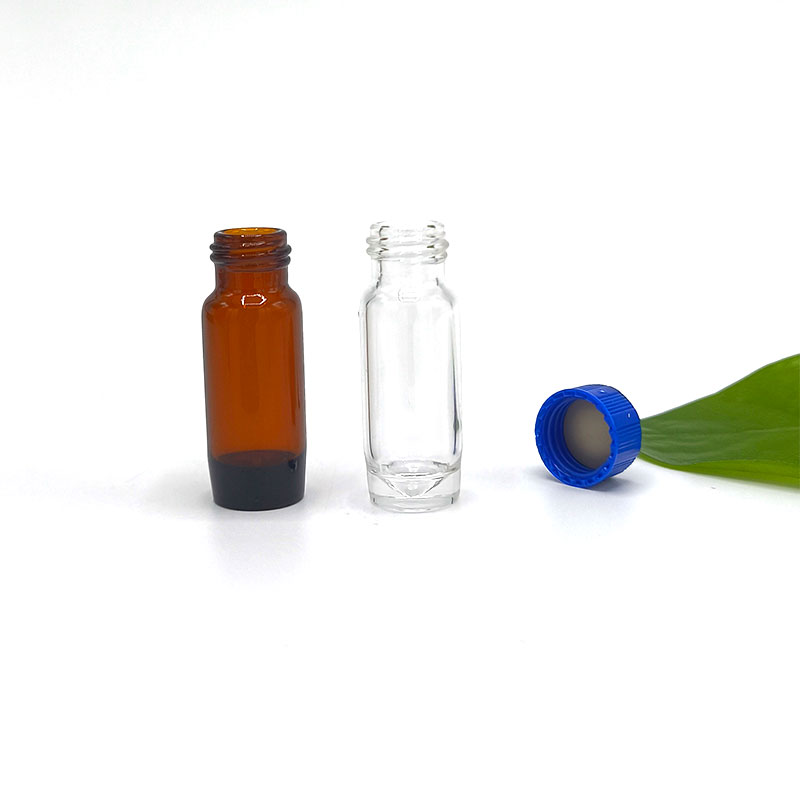
Narrow Mouth Reagent Bottle

Why Glass Packaging Continues to Play a Critical Role in the Industry

Excellent Chemical Stability for Sensitive Materials

Glass has long been valued in pharmaceutical applications because of its stable physical and chemical characteristics. Unlike some alternative materials, high-quality glass provides reliable resistance against many acids, solvents, and reactive substances. This property helps reduce the risk of unwanted reactions between the container and stored materials.

For laboratories working with demanding formulations, packaging stability is directly connected with research accuracy and product safety. A well-designed glass container can help preserve the original characteristics of chemical solutions, reagents, and pharmaceutical compounds during storage periods.

Protection Through Advanced Manufacturing Technology

The production of pharmaceutical glass containers requires strict control throughout the manufacturing process. From raw material selection and glass forming to surface treatment and quality inspection, every stage influences the final performance of the container.

Manufacturers are continuously improving production technologies to achieve better dimensional accuracy, stronger mechanical performance, and more consistent quality. These improvements support the growing need for dependable packaging solutions across global pharmaceutical and laboratory markets.

Key Features That Define High-Quality Reagent Packaging

A professional laboratory container is not only a storage tool but also an important protection system. Its design must consider usability, safety, and compatibility with different applications. The following characteristics are commonly valued in advanced glass packaging solutions.

Feature Industry Value
Stable glass material Helps maintain chemical purity and storage reliability
Secure sealing structure Supports contamination prevention and safer handling
Clear appearance Allows convenient observation of stored substances
Flexible customization Meets different laboratory and pharmaceutical requirements

Market Trends Driving Innovation in Pharmaceutical Containers

The global pharmaceutical packaging market is moving toward higher standards of safety, precision, and customization. Research organizations and manufacturers are looking for packaging partners that can provide not only reliable products but also technical support and flexible production capabilities.

Environmental considerations are also influencing the development of glass packaging. Because glass can be recycled and reused through established processes, it remains an attractive material for industries seeking sustainable packaging approaches. At the same time, improvements in manufacturing efficiency are helping companies balance quality requirements with responsible production practices.

Customization Becomes an Important Competitive Advantage

Different industries often require different packaging specifications based on application conditions. Factors such as bottle shape, closure compatibility, surface treatment, and labeling requirements can influence the effectiveness of the final solution.

Professional manufacturers are focusing on customized services to support diverse customer needs. This approach allows pharmaceutical companies, laboratories, and chemical enterprises to obtain packaging solutions that better match their operational processes.

How Reliable Packaging Supports Pharmaceutical and Research Applications

Packaging performance has a direct influence on the safety and efficiency of laboratory operations. Containers used for chemical reagents and pharmaceutical materials must provide dependable protection from external influences while maintaining convenient handling characteristics.

Narrow Mouth Reagent Bottle products are designed with controlled dispensing and secure storage in mind. The narrow opening helps reduce unnecessary exposure during usage, while the glass structure supports long-term stability for many applications. These characteristics make this type of container suitable for professional environments requiring accuracy and consistency.

Quality Control Strengthens Industry Confidence

Quality management is a fundamental part of pharmaceutical packaging manufacturing. Reliable suppliers establish comprehensive inspection procedures to ensure that containers meet expected standards for appearance, strength, sealing performance, and cleanliness.

Continuous improvement in production management also helps manufacturers respond to changing market expectations. Companies with strong technical capabilities and manufacturing experience can provide more dependable support for global industries.

Future Development Direction of Glass Reagent Packaging

As pharmaceutical research and chemical applications continue expanding, demand for specialized glass packaging will remain strong. Future development will focus on improving material performance, optimizing production processes, and providing more adaptable solutions for different application environments.

Innovation will not only involve product design but also include service capabilities. Manufacturers that understand industry challenges and provide complete packaging solutions will have stronger opportunities to build long-term cooperation with international markets.

Cangzhou Kangbo Pharmaceutical Packaging Co., Ltd. Supports Global Packaging Needs

Cangzhou Kangbo Pharmaceutical Packaging Co., Ltd. is dedicated to providing high-quality glass packaging solutions for pharmaceutical, chemical, and scientific research industries. With a strong understanding of packaging safety and manufacturing precision, the company focuses on delivering reliable products, customized services, and consistent quality control.

By combining advanced production capabilities with professional industry experience, Cangzhou Kangbo Pharmaceutical Packaging Co., Ltd. continues to serve as a trusted partner for customers seeking dependable glass packaging solutions. The company remains committed to protecting product safety, supporting scientific development, and creating long-term value through professional manufacturing expertise.

Related News
Leave me a message
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.Privacy Policy
RejectAccept